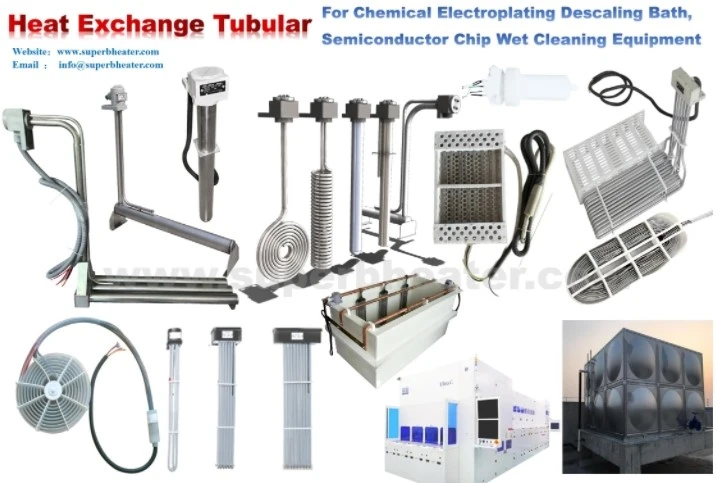
A heating plate installed in a chemical tank may have adequate rated power but still produce uneven bath temperatures. One common reason is often overlooked during equipment design: tank bottom geometry.
A flat-bottom tank, sloped tank, stepped bottom, or tank with internal supports creates different liquid depths and flow paths around the heating surface. These differences affect convection, heat distribution, and temperature measurement.
For chemical processing equipment, heating plate geometry should therefore be matched to the tank bottom rather than treated as an independent component.
Why Tank Shape Changes Heat Distribution
Heat released by a heating plate must move through the surrounding liquid.
Natural convection occurs as heated liquid becomes less dense and rises. The resulting flow depends strongly on available space beneath and around the heating surface.
A flat tank bottom with sufficient clearance can support relatively even circulation. A sloped or irregular bottom may create shallow regions where liquid movement is restricted.
These stagnant areas can develop different temperatures from the main bath.
The basic heat-transfer relationship is:
Q = hAΔT
When circulation becomes weaker, the effective heat-transfer coefficient h can decrease. A larger temperature difference may then be required to transfer the same heating power.
Shallow Zones Are Particularly Sensitive
A heating plate positioned near a shallow section of the tank bottom may have less liquid volume available to absorb heat.
If the same electrical power is concentrated into this region, local temperature can increase more rapidly.
Surface heat flux provides a useful engineering indicator:
q″ = Q/A
Reducing heat flux through a larger active area can help, but geometry still matters. A large heating plate installed across an uneven bottom may itself experience non-uniform liquid coverage.
The design objective is therefore not simply maximum heating area. The heating surface must remain effectively covered and accessible to sufficient liquid circulation.
Matching Plate Layout to Tank Geometry
Different tank-bottom structures require different heating plate arrangements.
| Tank bottom condition | Main thermal challenge | Suitable layout consideration | Temperature-uniformity priority |
|---|---|---|---|
| Flat bottom | Relatively uniform flow | Broad heating area | Moderate |
| Sloped bottom | Unequal liquid depth | Geometry-matched placement | High |
| Stepped bottom | Multiple thermal zones | Separate heating sections | High |
| Narrow channel | Restricted circulation | Elongated heating area | High |
| Bottom with supports | Flow obstruction | Clearance around supports | High |
The table shows why tank geometry should be included in the heating plate specification before dimensions and power are finalized.
Multiple Heating Zones Can Solve Uneven Geometry
For a large or irregular tank, one large heating plate may not provide the best temperature distribution.
Multiple independently controlled heating sections can compensate for different thermal zones. A section located in a deeper region may require a different heating load from one installed near a shallow area.
This arrangement also provides better control during partial tank filling.
When the liquid level changes, individual heating zones can be controlled according to the actual wetted area. This can reduce the risk of excessive local heat flux during low-volume operation.
PTFE Requires Careful Heat Distribution
In corrosive chemical tanks, a PTFE heating plate may be selected for its chemical resistance. However, PTFE has relatively low thermal conductivity compared with common metals.
As a result, internal heating-element spacing and surface area become important design factors.
An irregular tank bottom can make this more challenging. If the heating element is concentrated in one region while liquid circulation is restricted by tank geometry, local thermal gradients may become more pronounced.
A geometry-matched design can distribute heating more effectively while maintaining the required chemical resistance.
Sensor Location Should Follow the Thermal Flow
Tank geometry also affects temperature sensor accuracy.
A sensor installed above a heating plate may detect warmer liquid before that heat has reached the rest of the tank. Conversely, a sensor located in a stagnant corner may respond too slowly.
For irregular tank bottoms, the sensor should be positioned according to the actual circulation pattern and the process-critical temperature zone.
In larger systems, comparing temperatures at different locations during commissioning can reveal thermal stratification that a single sensor cannot detect.
Practical Design Checks
Before specifying a heating plate for a non-standard tank, several dimensions should be reviewed:
Bottom slope and step height
Available heating clearance
Minimum and maximum liquid depth
Heating plate mounting position
Circulation direction
Internal obstructions
Required temperature uniformity
Normal and minimum operating volume
These details help determine whether one heating zone is sufficient or whether a distributed configuration would provide better control.
Geometry Should Be Part of the Heating Plate Specification
Tank bottom geometry directly influences liquid depth, convection, heat transfer, and sensor response. Ignoring these factors can result in a heating plate that has sufficient electrical capacity but poor real-world temperature uniformity.
For irregular chemical tanks, the better approach is to match heating area, power density, plate position, circulation, and control zones to the actual bottom geometry.
When designing or replacing a heating plate, drawings or dimensional data for the tank bottom can significantly improve the accuracy of the thermal design and help establish a configuration suited to the actual operating conditions.